
By the end of this chapter, you will be able to:
Mastering these skills ensures you work safely and produce quality welds that meet real-world industry standards.
Gas Metal Arc Welding (GMAW) is a widely used welding process in Kenya's manufacturing and fabrication industries, especially in metal workshops servicing automotive, construction, and agricultural sectors. Metal Active Gas (MAG) welding, a variant of GMAW, uses active gases to enhance weld penetration and quality on ferrous metals. Understanding the equipment and gases involved is crucial for welding professionals to produce durable, defect-free joints that meet Kenya’s industrial standards.
MAG welding requires specialized equipment designed to deliver controlled electrical energy and shielding gases for effective welding. The choice of equipment influences weld quality, efficiency, and safety, which are critical in Kenyan workshops and fabrication plants producing structural components and machinery parts.
Active gas cylinders store and supply the shielding gases essential for MAG welding. An active gas reacts slightly with the molten pool, which stabilises the arc and increases penetration on steel. Proper selection, handling, and maintenance of these cylinders ensure consistent gas flow and prevent contamination, which could compromise weld integrity.
The gas in the cylinder is chosen to suit the metal, the thickness, and the quality of finish required. The cylinder size and type are then chosen to suit the volume of welding in the workshop or on site. The main uses are listed below.
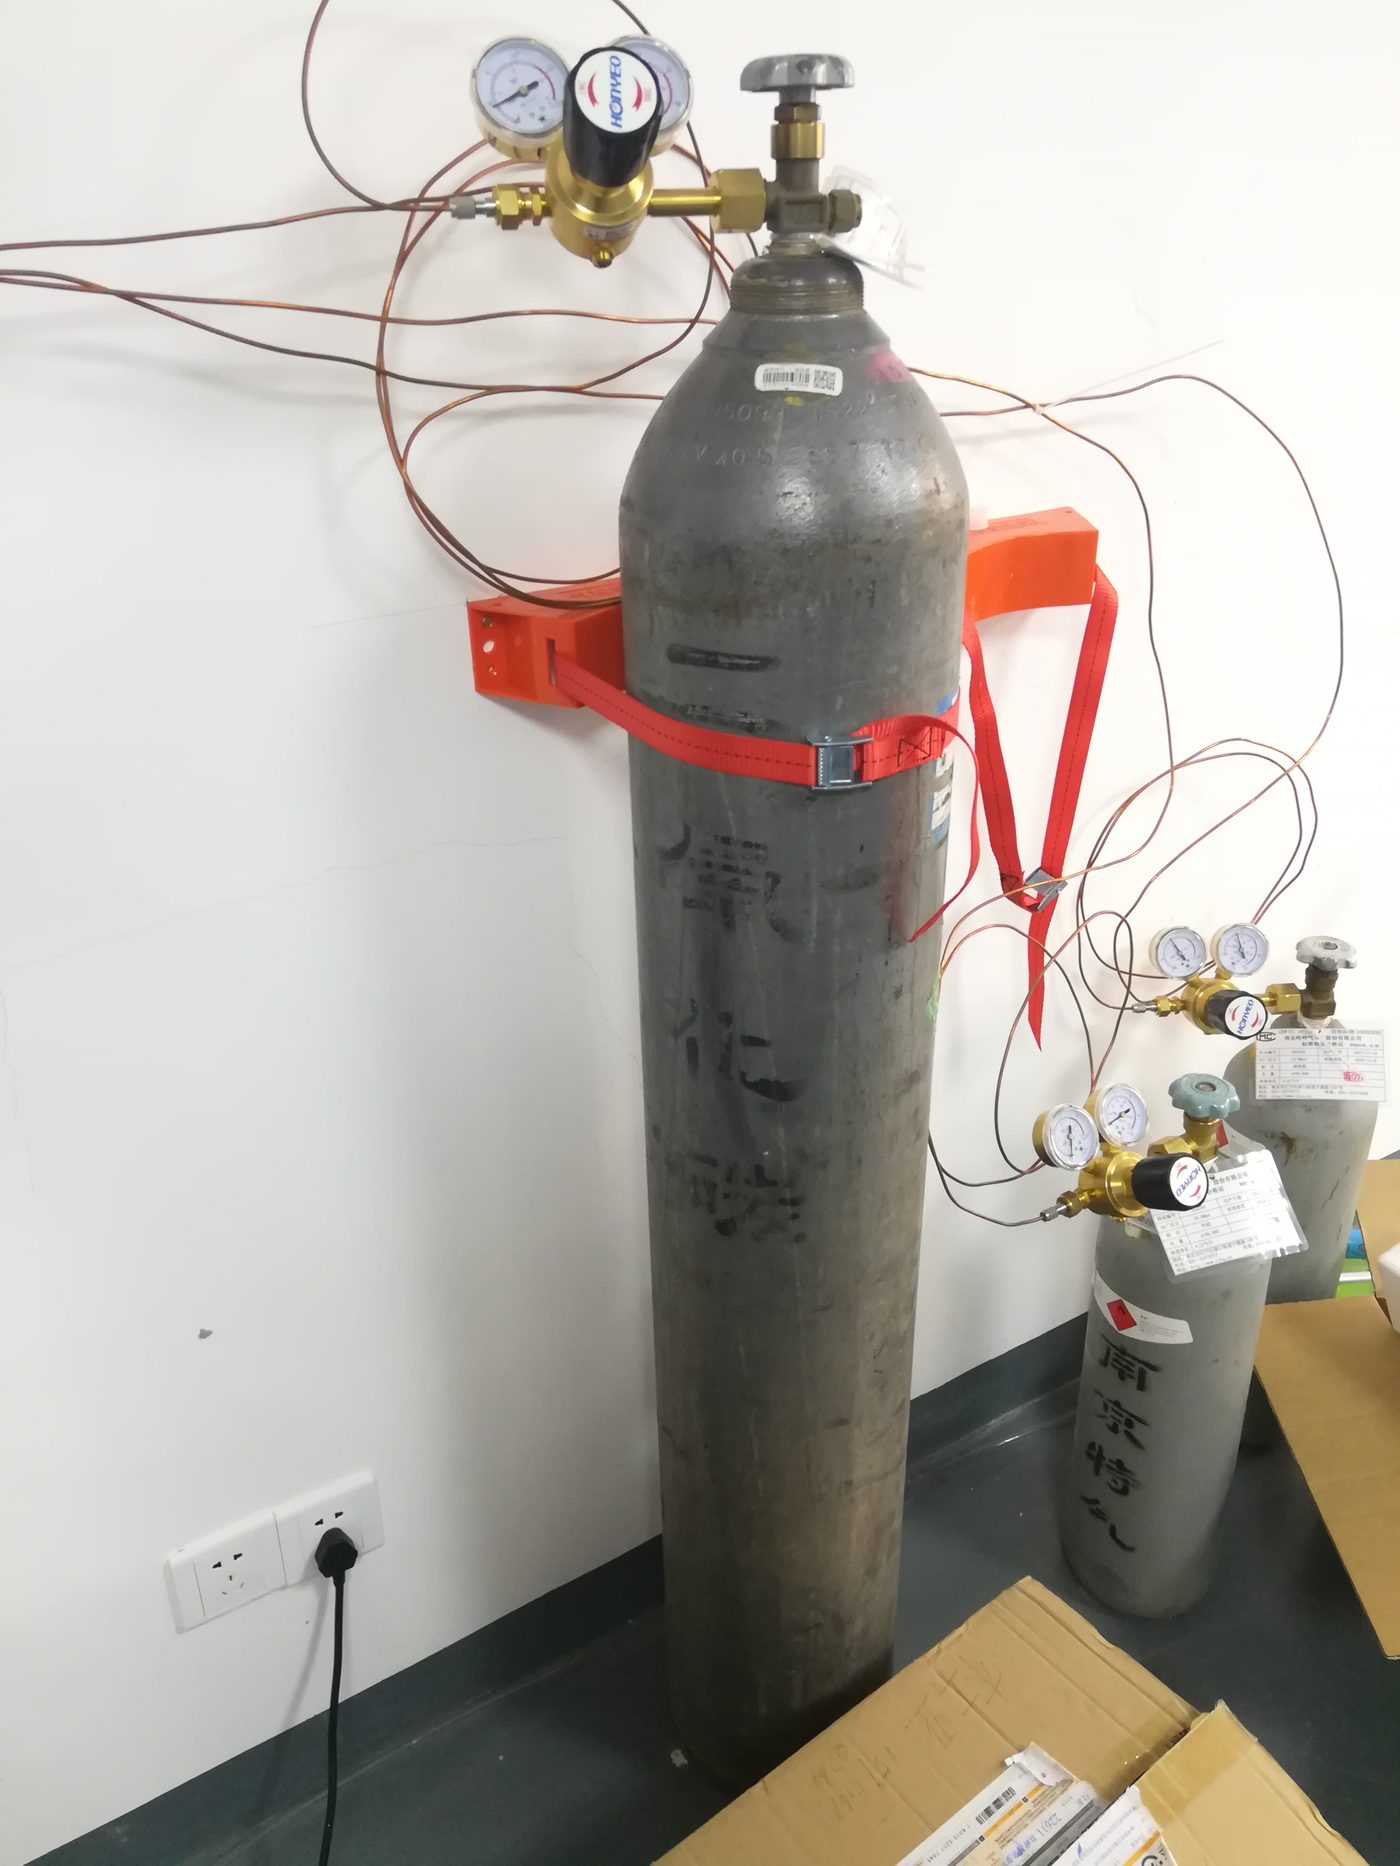
Carbon dioxide cylinder for welding use (Source: Wikimedia Commons)
Cylinder sizes are chosen to suit the work:
Cylinders hold gas at high pressure, so careless handling can cause injury, fire, or damage to the equipment. Good care also protects weld quality, because damaged valves, leaking fittings, and contaminated gas lines allow air into the weld zone and cause porosity.
Safe handling and storage:
Regulator and flowmeter care:
Cylinder connection and maintenance procedure:
MAG welding requires a stable power source and a wire feeder that feeds the consumable electrode wire consistently into the weld pool. The power source supplies a constant voltage, and the wire feeder sets the wire speed, which controls the welding current. Inverter-based power sources are light and energy efficient, which suits mobile workshops and site work.
The welding torch delivers current, shielding gas, and wire to the weld joint. Ergonomic design reduces operator fatigue, which is important in fabrication shops where welders may work extended hours. Cable assemblies must be properly insulated and maintained to prevent electrical hazards.
Additional equipment such as earth clamps, gas hoses, contact tips, nozzles, and protective gear are integral to MAG welding operations. Workshops must keep these accessories in good condition to ensure safety and welding quality. Example: a small fabrication workshop that uses its welding set only occasionally should still inspect the earth clamp and hoses before every job.
| Name | Specification | Use |
|---|---|---|
| Earth (work) clamp | Copper alloy or brass jaws with a firm spring grip and a cable of adequate size | Completes the welding circuit by connecting the workpiece to the power source |
| Gas hose | Flexible hose rated for the gas, free from cracks, with secure clamps | Carries shielding gas from the regulator to the wire feeder and torch |
| Contact tips | Copper alloy, bore matched to wire diameter (for example 0.8, 1.0, 1.2 mm) | Transfer current to the wire and guide it into the arc |
| Nozzles | Copper or brass, sized to the joint access | Direct a smooth gas shield over the weld pool |
| Welding helmet | Auto-darkening or fixed filter lens of suitable shade | Protects eyes and face from arc radiation and spatter |
| Gloves, apron, and boots | Leather or flame-resistant material | Protect the body from heat, sparks, and spatter |
| Chipping hammer and wire brush | Steel tools of suitable size | Clean spatter and prepare the joint and finished weld |
Create a free account to open more of this chapter.
Free: practical guides, quick cards, workplace scenarios and more.
Create a free accountThis chapter provided a comprehensive overview of Metal Active Gas welding, focusing on the equipment and accessories essential for effective MAG welding operations. It detailed the types and applications of active gas cylinders, emphasizing proper care to ensure safety and functionality. The role of shielding gases, particularly carbon IV oxide, was explored to highlight their importance in protecting the weld from atmospheric contamination. The chapter then examined the MAG welding process itself, outlining the step-by-step procedure necessary for successful welds. Practical applications were discussed, demonstrating how to perform MAG welding on various metals including steel, aluminium, copper, and titanium with thicknesses ranging from 4 to 16 millimeters. The integration of theory and practice was designed to equip learners with the skills to carry out MAG welding confidently and competently in diverse industrial contexts.
Type: Individual
| Tools & Equipment | Materials |
|---|---|
| Metal Active Gas (MAG) welding machine and accessories | Mild steel welding wire 0.8 mm diameter |
| Welding helmet | Argon-CO2 active gas cylinder (80% Argon, 20% CO2) |
| Leather gloves | |
| Safety boots | |
| Welding apron | |
| Angle grinder | |
| Wire brush | |
| Chipping hammer | |
| Steel rule 300 mm | |
| Vernier caliper | |
| Scriber | |
| Try square | |
| Work holding device (clamps) | |
| Welding bench |
| S/N | Item | Quantity |
|---|---|---|
| 1 | Metal Active Gas (MAG) welding machine and accessories | 1 set per candidate |
| 2 | Mild steel welding wire 0.8 mm diameter | 50 meters per candidate |
| 3 | Argon-CO2 active gas cylinder (80% Argon, 20% CO2) | 1 cylinder per 5 candidates |
| 4 | Welding bench | 1 per candidate |
| 5 | Work holding device (clamps) | 2 per candidate |
| 6 | Welding helmet | 1 per candidate |
| 7 | Leather gloves | 1 pair per candidate |
| 8 | Safety boots | 1 pair per candidate |
| 9 | Welding apron | 1 per candidate |
| 10 | Angle grinder | 1 per 5 candidates |
| 11 | Wire brush | 1 per candidate |
| 12 | Chipping hammer | 1 per candidate |
| 13 | Steel rule 300 mm | 1 per candidate |
| 14 | Vernier caliper | 1 per 5 candidates |
| 15 | Scriber | 1 per candidate |
| 16 | Try square | 1 per candidate |
| Items to be Evaluated | Marks Available | Marks Obtained | Comments |
|---|---|---|---|
| TASK 1: Adherence to safety procedures | |||
| Wearing welding helmet (Award 1 mark for wearing helmet, 0 if not) | 1 | ||
| Wearing safety boots (Award 1 mark for wearing boots, 0 if not) | 1 | ||
| Wearing leather gloves (Award 1 mark for wearing gloves, 0 if not) | 1 | ||
| Wearing welding apron (Award 1 mark for wearing apron, 0 if not) | 1 | ||
| Sub-Total | 4 | ||
| TASK 2: MAG welding machine setup | |||
| Placed welding machine on dry and stable surface (Award 1 mark if machine placed correctly, 0 if not) | 1 | ||
| Connected welding cables and wire feeder correctly (Award 1 mark if cables and feeder connected properly, 0 if not) | 1 | ||
| Set welding current to suit 5 mm thick mild steel (approx. 120-140 amps) (Award 1 mark if current set correctly, 0 if not) | 1 | ||
| Set active gas flow rate to 15-20 liters per minute for 5 mm plate (Award 1 mark if gas flow rate set correctly, 0 if not) | 1 | ||
| Opened gas cylinder valve fully and checked for leaks (Award 1 mark if valve opened fully and no leaks, 0 if not) | 1 | ||
| Switched on machine and checked wire feed operation (Award 1 mark if machine started and wire feeds properly, 0 if not) | 1 | ||
| Switched off machine when setup complete (Award 1 mark if machine switched off after setup, 0 if not) | 1 | ||
| Closed gas cylinder valve after setup (Award 1 mark if gas valve closed after setup, 0 if not) | 1 | ||
| Hung up welding blowpipe safely after use (Award 1 mark if blowpipe hung correctly, 0 if not) | 1 | ||
| Sub-Total | 9 | ||
| TASK 3: Housekeeping | |||
| Cleaned the work station of debris and slag (Award 1 mark if area cleaned, 0 if not) | 1 | ||
| Disposed waste correctly in designated bins (Award 1 mark if waste disposed properly, 0 if not) | 1 | ||
| Returned machine and accessories to correct storage locations (Award 1 mark if items returned properly, 0 if not) | 1 | ||
| Sub-Total | 3 | ||
| PRODUCT CHECKLIST | |||
| Welding machine and accessories correctly set for 5 mm plate welding (current, wire speed, gas flow) (Award 1 mark each for correct current, wire speed, and gas flow settings) | 3 | ||
| All connections secure and no gas leaks detected (Award 2 marks if connections secure and no leaks, 0 otherwise) | 2 | ||
| Welding blowpipe and cables properly arranged and safe (Award 1 mark if blowpipe and cables are properly arranged) | 1 | ||
| Workstation clean and free of hazards (Award 2 marks if workstation is clean and hazard free) | 2 | ||
| Sub-Total | 8 | ||
| GRAND TOTAL | 24 | ||
Type: Individual
| Tools & Equipment | Materials |
|---|---|
| Regulator with dual gauges for active gas cylinder | Carbon dioxide (CO2) cylinder 10kg |
| Gas hose (3 meters) | Leak detection solution (soap water) |
| Welding blowpipe with connector | |
| Spanner set | |
| Cylinder trolley |
| S/N | Item | Quantity |
|---|---|---|
| 1 | Oxygen cylinder 10kg | 1 Pc per Candidate |
| 2 | Carbon dioxide (CO2) cylinder 10kg | 1 Pc per Candidate |
| 3 | Regulator with dual gauges for active gas cylinder | 1 Pc per Candidate |
| 4 | Gas hose (3 meters) | 1 Pc per Candidate |
| 5 | Welding machine (MAG type) with accessories | 1 set per 5 Candidates |
| 6 | Welding blowpipe with connector | 1 Pc per Candidate |
| 7 | Welding helmet | 1 Pc per Candidate |
| 8 | Leather gloves | 1 Pair per Candidate |
| 9 | Safety boots | 1 Pair per Candidate |
| 10 | Welding apron | 1 Pc per Candidate |
| 11 | Leak detection solution (soap water) | 1 Bottle per 5 Candidates |
| 12 | Cylinder trolley | 1 Pc per 5 Candidates |
| 13 | Spanner set | 1 Set per 5 Candidates |
| Items to be Evaluated | Marks Available | Marks Obtained | Comments |
|---|---|---|---|
| TASK 1: Safety and Personal Protective Equipment | |||
| Wore welding helmet (Award 1 mark for wearing welding helmet, 0 if not) | 1 | ||
| Wore leather gloves (Award 1 mark for wearing leather gloves, 0 if not) | 1 | ||
| Wore safety boots (Award 1 mark for wearing safety boots, 0 if not) | 1 | ||
| Wore welding apron (Award 1 mark for wearing welding apron, 0 if not) | 1 | ||
| Sub-Total | 4 | ||
| TASK 2: Handling and Transporting Active Gas Cylinders | |||
| Used cylinder trolley to move CO2 cylinder safely (Award 1 mark for safe use of trolley, 0 if not) | 1 | ||
| Checked cylinder for damage and expiry date (Award 1 mark for inspection before use, 0 if not) | 1 | ||
| Kept cylinder in upright position during handling (Award 1 mark for correct cylinder orientation, 0 if not) | 1 | ||
| Sub-Total | 3 | ||
| TASK 3: Connecting Cylinder to MAG Welding Machine | |||
| Checked regulator and hose for damage before connection (Award 1 mark for inspection, 0 if not) | 1 | ||
| Connected regulator securely to CO2 cylinder using correct spanner (Award 1 mark for secure connection, 0 if not) | 1 | ||
| Attached gas hose securely to regulator and welding machine (Award 1 mark for proper hose connection, 0 if not) | 1 | ||
| Opened cylinder valve slowly and fully (Award 1 mark for correct valve operation, 0 if not) | 1 | ||
| Adjusted regulator pressure to 16-18 cubic feet per hour (cfh) (Award 1 mark for correct pressure setting, 0 if not) | 1 | ||
| Checked all connections for leaks using leak detection solution (Award 1 mark for leak test, 0 if not) | 1 | ||
| Sub-Total | 6 | ||
| TASK 4: Shutdown and Maintenance of Active Gas Cylinder Setup | |||
| Closed cylinder valve fully after welding (Award 1 mark for closing valve, 0 if not) | 1 | ||
| Released pressure from regulator and hose (Award 1 mark for releasing pressure, 0 if not) | 1 | ||
| Disassembled regulator and hose carefully (Award 1 mark for careful disassembly, 0 if not) | 1 | ||
| Stored cylinder in designated safe area upright with chain restraint (Award 1 mark for proper storage, 0 if not) | 1 | ||
| Sub-Total | 4 | ||
| TASK 5: Housekeeping | |||
| Cleaned work station after task completion (Award 1 mark for cleaning workstation, 0 if not) | 1 | ||
| Disposed waste and empty containers correctly (Award 1 mark for correct waste disposal, 0 if not) | 1 | ||
| Returned tools and accessories to their proper places (Award 1 mark for proper tool return, 0 if not) | 1 | ||
| Sub-Total | 3 | ||
| PRODUCT CHECKLIST | |||
| Cylinder connected securely without leaks at regulator and hose joints (Award 1 mark for each leak-free connection point) | 3 | ||
| Regulator pressure set correctly between 16 and 18 cfh (Award 2 marks for correct pressure setting, 0 if outside range) | 2 | ||
| Cylinder stored upright with safety chain and proper signage (Award 2 marks for correct storage, 0 if not) | 2 | ||
| No visible damage or defects on cylinder and accessories (Award 2 marks for defect-free equipment, 0 if defects present) | 2 | ||
| Sub-Total | 9 | ||
| GRAND TOTAL | 29 | ||
At the start of this chapter we promised you would be able to:
Tick each one you can genuinely do.
So, are you there yet?
You're competent when you can confidently do 50% or more of what this chapter promised.
Sign in to record how you're doing.